
Preventing Drill Tool Fracture: Lessons from 23CrNi3Mo Steel Failure Analysis
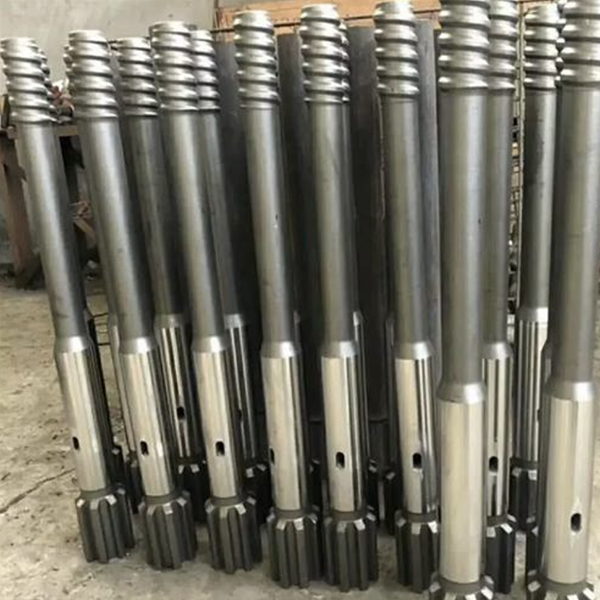
Drill tools used in mining, quarrying and energy projects operate under some of the harshest mechanical conditions in industry. DTH hammer components, shanks, drill rods and bit bodies must withstand repeated impact, torsion, bending, abrasive wear, corrosion and contact stress. When a tool fractures prematurely, the result is more than the loss of one component: drilling stops, production is delayed and connected equipment may be damaged.
Failure analysis of carburized 23CrNi3Mo steel drill tools provides valuable guidance for manufacturers and users. The key lesson is that fatigue life depends on the balance between surface hardness and core toughness, as well as machining accuracy, heat treatment and overall material quality.
Why Drill Tools Are Vulnerable to Fatigue Failure
A drill tool is exposed to repeated loading during every drilling cycle. Impact energy travels through the tool body, while rotation and feed force create additional stress. In real working conditions, the component may also experience:
Bending from misalignment or hole deviation.
Torsional loading from rotation and bit-rock contact.
Abrasive wear from rock dust and cuttings.
Corrosion from mine water, flushing water or wet drilling conditions.
Local stress concentration at splines, threads, shoulders and machined transitions.
These loads are not static. They repeat thousands of times during drilling, which makes fatigue performance critical. Small surface defects, sharp machining marks, poor transitions or unsuitable heat treatment can become crack-initiation sites. Once a crack forms, impact loading can drive it forward rapidly.
The Role of Carburizing in Drill Tool Performance
Carburizing is commonly used to create a hard, wear-resistant surface while retaining a tougher core. For drill tools, this combination is essential. The surface must resist wear and contact damage, while the core must absorb impact energy and prevent brittle fracture.
A successful carburized structure should have a gradual transition from the hard surface layer to the softer, tougher core. This hardness gradient helps distribute stress and reduces the risk of a sudden property change between layers.
If the carburized layer is too brittle, too uneven or poorly matched to the core, fatigue resistance can decline. A narrow transition zone may create a sharp change in hardness and microstructure. Under repeated impact, this region can become vulnerable to cracking. In contrast, a broader and smoother transition helps the tool resist crack initiation and slows crack propagation.
Fracture Appearance Helps Identify the Root Cause
Fracture-surface examination is one of the most useful methods in drill-tool failure analysis. Scanning electron microscopy can reveal whether a crack grew gradually through fatigue or whether the component fractured suddenly.
A component with better fatigue resistance often shows evidence of crack growth before final failure, including fatigue striations and ductile dimples. These features indicate that the material absorbed energy and resisted crack propagation over time.
By comparison, a brittle fracture may appear relatively smooth and show limited plastic deformation. This can indicate that a defect or stress concentration led to rapid fracture before the material had an opportunity to deform significantly.
The location of the failure is also important. Splines, thread roots and sharp geometric transitions are common locations for stress concentration. If fractures consistently start at a spline edge or machined corner, the investigation should focus on surface finish, dimensional accuracy, tool geometry and local heat-treatment effects.
Microstructure and Hardness Must Work Together
A hard surface is not automatically a durable surface. Drill-tool reliability depends on the relationship between the carburized layer, transition zone and core structure.
For many impact-drilling components, the desired structure combines a high-hardness surface with a core that maintains sufficient toughness. A gradual hardness profile can help reduce brittle behavior. The microstructure should be controlled to avoid excessive brittleness while providing adequate resistance to wear and deformation.
Martensitic structures can deliver high hardness, but excessive hardness in the core or an abrupt transformation zone may reduce toughness. Bainitic or tempered structures in the core can help support impact resistance, depending on the specific design and heat-treatment process.
The correct result is not one universal hardness value. It is a controlled property profile that matches the tool geometry, alloy composition, operating load and expected wear conditions.
Steel Cleanliness Still Matters
Non-metallic inclusions can become fatigue initiators when they are large, poorly distributed or located near highly stressed surfaces. Oxide and sulfide inclusions should therefore be controlled through clean steelmaking practice.
However, the presence of small inclusions does not automatically explain every failure. If inclusions are fine and well controlled, the more important cause may be heat-treatment imbalance, poor transition-zone design, surface defects or machining damage.
A complete failure investigation should examine:
Fracture origin and crack-growth direction.
Surface and subsurface microstructure.
Carburized-case depth and hardness gradient.
Core hardness and toughness indicators.
Inclusion size, type and distribution.
Geometry of splines, threads and shoulders.
Machining marks, grinding burns and surface roughness.
Actual drilling conditions and maintenance records.
Manufacturing Controls That Improve Tool Life
Improving drill tool life requires coordinated quality control from raw material to final inspection.
Steel production should control composition, cleanliness and segregation. Rolling and forging should maintain uniform microstructure and avoid coarse-grain regions. Machining should minimize sharp notches, deep tool marks and irregular surface finishes. Critical surfaces should be inspected before heat treatment and again before shipment.
Carburizing and subsequent heat treatment require especially careful control. Case depth, carbon potential, quenching rate and tempering conditions all influence the final microstructure and hardness profile. A robust process produces a wear-resistant surface, a smooth transition zone and a tough core.
Manufacturers should also use process validation methods such as hardness traverses, metallographic examination, dimensional inspection and fatigue-related testing for critical products.
Practical Steps for Users
Drilling contractors can also reduce premature failures through correct operation. Tools should be matched to the drill’s impact energy, torque and hole diameter. Worn couplings, poor alignment and excessive feed force should be corrected early. Operators should inspect splines, threads and contact surfaces regularly, and remove damaged tools before cracks become catastrophic failures.
The goal is not merely to make a drill tool harder. The goal is to create a component with the right balance of wear resistance, toughness, fatigue resistance and manufacturing precision. For 23CrNi3Mo drill tools, that balance is the foundation of reliable, long-life performance in demanding rock-drilling environments.



